If you work in water distribution, gas transmission, or any industry relying on seamless, long-lasting pipe networks, you’ve probably encountered PE (polyethylene) butt fusion fittings. As a supplier of these fittings, I’ve seen firsthand how a small misstep in installation can turn a reliable system into a costly headache—leaks, pressure drops, or even full system failures. That’s why I’m breaking down this process step by step, drawing on 12 years in the industry and hundreds of successful installations across North America. No fluff, no overly technical jargon just to sound smart—just practical, actionable guidance that even first-time installers can follow. PE Buttfusion Fittings
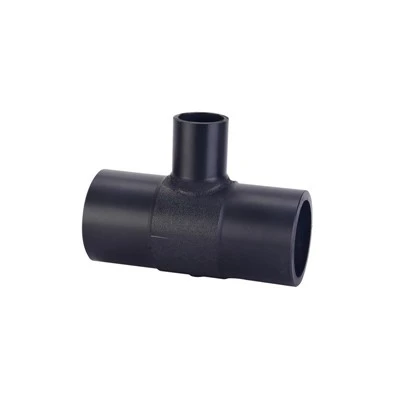
First, let’s get clear on what PE butt fusion fittings are and why they matter. Unlike threaded or solvent-welded fittings, which can weaken over time or fail under high pressure, butt fusion creates a molecular bond between two PE surfaces. It’s like fusing two pieces of the same material together so seamlessly, you can barely tell where one ends and the other begins. This makes it ideal for underground pipelines, municipal water lines, and industrial gas systems where durability and leak resistance are non-negotiable.
Before we dive into the installation steps, a quick note on safety and prep. I always tell my clients: the best installation starts long before you turn on the fusion machine. First, confirm you have the right tools. You’ll need a butt fusion machine calibrated for the diameter of your pipe and fittings, a scribe or marker, a faced cutter to trim pipe ends, a heater plate, a pressure gauge, a beveller, and a clean cloth (no oil or grease—PE hates contaminants). Next, inspect every component: check fittings for scratches, dents, or manufacturing defects, and confirm your pipe matches the fitting’s diameter and PE grade (most modern fittings are PE 100, the industry standard for high stress applications). A mismatched grade could lead to a weak bond, so double-check specifications before you start.
Now, let’s walk through the step-by-step process, the way we teach it to our installation partners.
Step 1: Align the Pipe and Fitting Proper Alignment is 90% of a successful fusion. If the two surfaces aren’t perfectly straight, you’ll get a lopsided weld that leaks under pressure. Start by clamping your pipe into the fusion machine’s vice, making sure it’s secured tightly and doesn’t wiggle. Then, bring the fitting into place, aligning it so the pipe end meets the fitting’s socket end evenly. Use a level to check for straightness—even a 1-degree angle can throw off the pressure later. Once aligned, tighten the vice completely, then double-check: hold a straight edge along the pipe and fitting, if there’s any gap between the edge and the surface, adjust until it’s flush.
Step 2: Face and Square the Surfaces Before you fuse, both ends need to be perfectly flat, clean, and square. A rough or uneven surface will prevent the heater plate from making consistent contact, leading to cold spots in the weld. Use the faced cutter that comes with your fusion machine to trim 0.5 to 1 mm off each end. Apply steady, even pressure as you cut—don’t rush, and don’t stop mid-cut. Once you’ve faced both ends, remove any loose PE shavings with a dry, lint-free cloth. Never use water or cleaning spray here—moisture or chemicals will contaminate the surface and ruin the bond. I once had a client skip this step and use a paper towel that had been sprayed with glass cleaner; the weld failed six months later, costing them $20,000 in repairs. That’s a mistake no one needs to make.
Step 3: Heat the Surfaces Now, the heating phase. This is where you bring the pipe and fitting to the right temperature—PE melts around 210 to 230 degrees Celsius, so calibrate your heater plate to that range. Once the heater is up to temperature, move it between the two faced ends, applying consistent pressure to create a melt bead. The bead should be uniform around the entire circumference of the fitting and pipe—any gaps or thin spots mean you’re not applying enough pressure, or the heater isn’t evenly heated. How long should you heat? A good rule of thumb is 1 minute for every 10 mm of diameter. For example, a 110 mm fitting needs 11 minutes of heating, a 200 mm fitting needs 20 minutes. Don’t overheat—if the surface turns brown or starts to drip, you’ll burn the PE, creating a weak, brittle weld. If you underheat, the bond won’t be molecular, and it will split under pressure later.
Step 4: Join the Pipe and Fitting Once the bead is uniform and the ends are fully melted, move the heater plate out of the way quickly (but carefully—don’t drag it across the surfaces, which would scrape the melt) and bring the two ends together. Apply pressure steadily until you get a consistent bead that squeezes out around the entire joint—this is called the “flash,” and it’s a good sign. The flash should be smooth and even, no lumps or gaps. Hold the pressure for at least 5 minutes for smaller diameters, up to 10 minutes for larger ones, to let the bond cool and set. Resist the urge to move the joint before it’s fully cool—disturbing it can cause cracks in the weld. I’ve seen installers yank a joint too early because they were in a hurry, only to find a hidden crack that led to a leak months later. Patience here saves you money and time in the long run.
Step 5: Inspect the Weld After cooling, it’s time to check your work. The flash should be uniform all around—if one side is missing or lopsided, that’s a red flag. You can also do a visual test: run your finger along the weld, it should feel smooth, with no cracks, pits, or irregularities. For larger systems, we recommend a pressure test after installation: fill the line with water and increase pressure gradually, checking for leaks around the joint. If the weld passes the visual and pressure tests, it’s ready to go. If not, you’ll need to cut it out and start over—don’t try to patch a bad weld.
Now, let’s talk about common mistakes we see all the time, and how to avoid them. First, using mismatched components. PE 80 and PE 100 fittings look similar, but their melting points and strength levels are different. Using a PE 80 fitting with PE 100 pipe will result in a weak bond. Always confirm the material grade on the pipe and fitting before you start. Second, not accounting for temperature. PE is sensitive to cold—if you’re installing in temperatures below 5 degrees Celsius, you’ll need to adjust your heating time by 20% and your cooling time by 30%. Cold PE melts faster, so you don’t want to overheat it. Third, skipping surface prep. Even a tiny bit of dirt or grease can create a weak spot. I always tell installers to wipe the ends one last time right before heating, just to be safe.
As a supplier, I also want to make sure you’re getting the right fittings for your application. We carry a full range of PE butt fusion fittings: 90-degree elbows, 45-degree elbows, tees, reducers, and end caps, all manufactured to meet ISO 4427 standards. We test every batch of fittings for strength and durability, so you can trust that when you receive our products, they’re ready to form a long-lasting bond with your pipe.
But here’s the thing: no matter how good your fittings are, a bad installation will ruin the job. That’s why we also offer on-site training for installation teams, walkthroughs of tough projects, and 24/7 support if you run into a problem mid-install. We’ve been working with contractors and municipal teams across the country for years, and we know that when you have the right tools, the right guidance, and high-quality fittings, PE butt fusion is one of the most reliable ways to build a pipe system.
If you’re planning a pipeline project, or you’re tired of dealing with leaky, low-pressure systems that fail on you, we’re here to help. Whether you need to confirm the right fitting size, get guidance on a tricky installation, or place a bulk order, our team is ready to assist.
PE Steel Transition Fittings References
- ISO 4427: Polyethylene (PE) pipes for water supply
- American Society for Testing and Materials (ASTM) D3350: Standard Specification for Polyethylene Plastics Pipe and Fittings Materials
- PE Pipe Systems Association: Best Practices for Butt Fusion Installation of Polyethylene Fittings
Zhejiang Shengbo Pipe Fittings & Valves Industry Co., Ltd.
With abundant experience, we are one of the most professional pe buttfusion fittings manufacturers and suppliers in China. Please feel free to buy discount pe buttfusion fittings from our factory. Welcome to contact us for quotation and free sample.
Address: No. 79 Hemudu North Road, Hemudu Town, Yuyao City, Ningbo City, Zhejiang Province, China
E-mail: shengbo@zj-shengbo.com
WebSite: https://www.shengbofitting.com/
