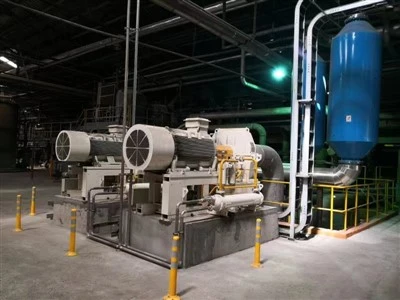
If you’ve ever worked with industrial vacuum systems—whether in food processing, pharmaceutical manufacturing, wastewater treatment, or mining—you’ve likely encountered a water ring vacuum pump. I’ve been supplying these pumps for over 12 years, and I can’t tell you how often new customers come to me assuming they’re “set it and forget it” workhorses, only to hit snags that lead to unplanned downtime, lost production, or even premature pump replacement. The truth is, water ring pumps are incredibly reliable, but like any precision piece of industrial equipment, they have specific vulnerable parts that, when neglected or misused, turn a solid investment into a headache. Today, I want to break down those vulnerable areas, what causes them to fail, and what you can do to extend the life of your pump—straight from the perspective of someone who installs, repairs, and services these units on a weekly basis. Water Ring Vacuum Pump
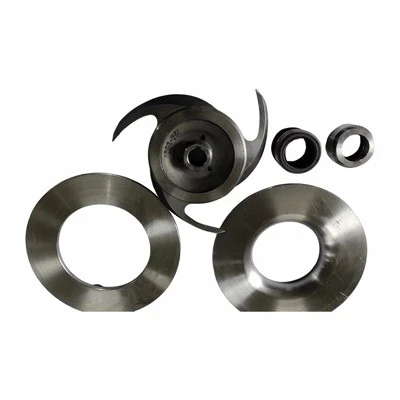
First, let’s start with the part that’s almost always the first to show wear: the mechanical seal. I’ve seen this fail in as little as six months on a pump that’s run nonstop, or last upwards of three years on a well-maintained unit. Mechanical seals on water ring pumps have two main components: a rotating face (usually silicon carbide or carbon) that spins against a stationary face, and a set of elastomer O-rings that create a tight, leak-proof barrier between the seal housing and the pump shaft. The problem here is two-fold. First, water ring pumps use process water (or sometimes recirculated seal water) that often contains tiny particulates—sediment, scale from hard water, or even small bits of debris from the process line. Those particulates act like sandpaper, grinding away at the seal faces every time the pump runs. Second, cavitation is a silent killer of mechanical seals in these pumps. Unlike oil-lubricated vacuum pumps, water ring pumps rely on the liquid ring itself to create the vacuum. If the inlet pressure drops too low, or the water temperature rises (because the pump is running too hard or the seal water isn’t cooled properly), the water in the pump starts to boil, forming tiny vapor bubbles. When those bubbles collapse, they create micro-shock waves that pitting the seal faces, leading to leaks. The telltale sign of a failing mechanical seal is water dripping from the seal housing—catch it early, and you can replace the seal for a few hundred dollars; wait until it’s completely failed, and you could be looking at shaft damage that costs thousands to repair.
Next on the list is the impeller. This is the heart of the water ring pump—it’s the curved, bladed rotor that spins inside the stationary casing, creating the liquid ring that draws in and compresses gas. Impellers are more durable than mechanical seals, but they’re still vulnerable, especially in pumps that handle dirty or abrasive process fluids. I once had a customer whose pump was handling raw sewage from a small food processing plant—within a year, the impeller blades were worn down so much that the pump could barely pull half the vacuum it was rated for. The culprit here was fine particulate matter in the sewage, which eroded the impeller blades over time. Even clean water can cause wear if the impeller is made of the wrong material—for example, a cast iron impeller will corrode if you’re pumping slightly acidic water, which eats away at the blade edges and disrupts the liquid ring’s shape. Another issue with impellers is misalignment during installation. If the impeller is not perfectly centered in the casing, it rubs against the casing wall every rotation, causing uneven wear on the blades and even cracks over time. I always tell new customers to insist on factory-trained technicians for pump installation—skimping on that step will almost always lead to impeller problems down the line.
The liquid ring itself might not seem like a part, but it’s the most critical component of the pump, and its condition is a huge vulnerable point. The liquid ring is the water (or sometimes other compatible liquid) that fills the pump casing and forms the vacuum barrier. Over time, this water gets contaminated with process gases, particulates, and even chemicals from the application. If you don’t recirculate or replace the liquid regularly, two things happen: first, the viscosity of the liquid changes—contaminated water is thinner than clean water, so it can’t form a tight, consistent ring, which reduces vacuum performance. Second, dissolved gases in the liquid can cause corrosion inside the casing and on the impeller, as I mentioned earlier. I had a pharmaceutical customer who was recirculating the same batch of water for six months straight because they thought it would save on water costs. By the time they called me, their pump casing was pitted with rust spots, and the liquid ring was so cloudy that the pump’s vacuum level dropped by 30%. The fix involved acid washing the casing, replacing the impeller, and implementing a weekly water change routine—something they’d skipped because they didn’t realize how big of an impact the liquid ring’s condition has.
Then there’s the suction and discharge valves, and the casing itself. Wait, the casing might seem like it’s indestructible, but that’s not always the case. Casing corrosion is another common vulnerable issue, especially in pumps used for chemical processing or wastewater applications. If the casing is made of standard cast iron, it will corrode if exposed to acidic or alkaline process fluids, leading to leaks and reduced structural integrity. I recently had a mining customer whose pump was handling a slurry with a pH of 4—after two years, the casing had developed a large pinhole leak at the bottom, which forced them to shut down their entire mineral processing line to repair it. The suction and discharge valves, which regulate the flow of gas into and out of the pump, are also vulnerable. These small, spring-loaded valves can get stuck open or closed if debris gets trapped under them, or if the spring wears out from constant use. When that happens, the pump can’t build proper pressure, or it backflows gas, reducing its efficiency. Most of the time, these valves are cheap to replace, but if you don’t check them during routine maintenance, they can lead to bigger problems.
I also want to talk about motor and coupling components, even though they’re not technically part of the pump’s vacuum-generating assembly. Wait, but in my line of work, these are often considered part of the water ring pump system, and they’re common points of failure that catch customers off guard. The motor that drives the impeller needs to be sized correctly for the application—if it’s underpowered, it will overheat and burn out when the pump is running at full capacity; if it’s overpowered, you’re wasting energy and putting unnecessary stress on the pump’s shaft. The coupling that connects the motor to the pump shaft is another weak point. Flexible couplings, which are designed to absorb minor misalignment, have rubber inserts that wear out over time, especially if the pump is subjected to frequent start-stop cycles or heavy vibration. I’ve seen couplings fail in as little as a year on pumps that start 10 times a day, leading to sudden shutdowns and even shaft damage.
So, now that we’ve covered the vulnerable parts, what can you do to protect your pump? From my experience, routine maintenance is non-negotiable. I recommend a weekly check: look for leaks at the mechanical seal, check the water level in the pump, listen for unusual noise (which could indicate cavitation or impeller rubbing), and inspect the suction and discharge valves. A monthly deep dive: drain and replace the liquid ring water, clean the strainers on the suction line, and check the coupling for wear. And an annual professional inspection: have a tech like me pull the pump apart, inspect the impeller for wear, check the casing for corrosion, and test the mechanical seal for durability. Also, make sure you’re matching the pump’s materials to your application—if you’re handling corrosive fluids, invest in a stainless steel casing and impeller instead of cast iron. If you’re dealing with abrasive materials, opt for a hard-coated impeller that can resist wear.
At the end of the day, a water ring vacuum pump is only as reliable as the care you put into it. I’ve seen customers run pumps for 10+ years with minimal issues, and I’ve seen others burn out a pump in six months because they skipped maintenance or used the wrong parts. If you’re currently experiencing problems with your water ring pump, or you’re looking to invest in a new unit that will stand up to your application’s demands, I’m here to help. We offer customized pump solutions, maintenance services, and replacement parts to keep your system running smoothly, no matter what industry you’re in. Don’t let a preventable part failure derail your production—reach out to me to discuss your needs and find the right solution for your operation.
Pulp Pump References:
- Huth, J. (2019). Water Ring Vacuum Pumps: Design, Operation, and Maintenance. Industrial Press.
- American Society of Mechanical Engineers (ASME). (2021). Standard for Maintenance of Vacuum Pump Systems. ASME International.
- Patel, R. (2022). "Wear Mechanisms in Water Ring Pumps for Industrial Applications." Journal of Industrial Fluid Machinery, vol. 130, no. 4, pp. 45-52.
- Van der Merwe, L. (2020). Cavitation Damage in Vacuum Pumps: Causes and Mitigation Strategies. Vacuum Technology Magazine.
- International Organization for Standardization (ISO). (2018). ISO 14856: Rotary Vacuum Pumps – Safety Requirements. ISO.
Xiaofeng Machinery Technology Co., Ltd.
As one of the most professional water ring vacuum pump manufacturers and suppliers in China, we also support custom service. Please feel free to wholesale advanced water ring vacuum pump made in China here from our factory. Quality products and reasonable price are available.
Address: No.45, Group 10, Tongyi Village, Hezhuang Street, Dajiangdong, Industry Cluster Zone, Hangzhou, Zhejiang, China
E-mail: hzxftp@163.com
WebSite: https://www.hzxfmt.com/
